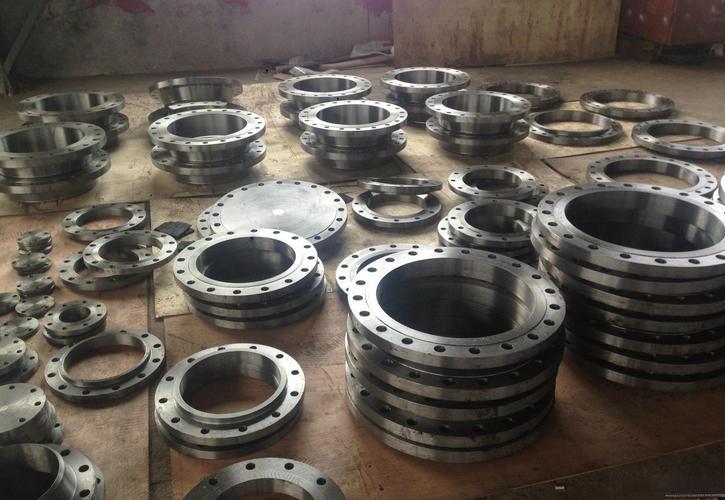
ASTM A350 LF2 forged flanges, UNS K03011, Class 1/2, Charpy tested at −46 °C/−18 °C. ASME B16.5/16.47, NPS 1/2–60. Low-temperature carbon steel, MTC 3.1.
ASTM A350 LF2 forged flanges, UNS K03011, Class 1/2, Charpy tested at −46 °C/−18 °C. ASME B16.5/16.47, NPS 1/2–60. Low-temperature carbon steel, MTC 3.1.
Heavy Industrial Specification Manual
Comprehensive Technical Datasheet: Chemical Composition, Mechanical Properties, ASME B16.49 Standards, Tolerances, and Dimensional Matrices for High-Yield Line Pipe Bends
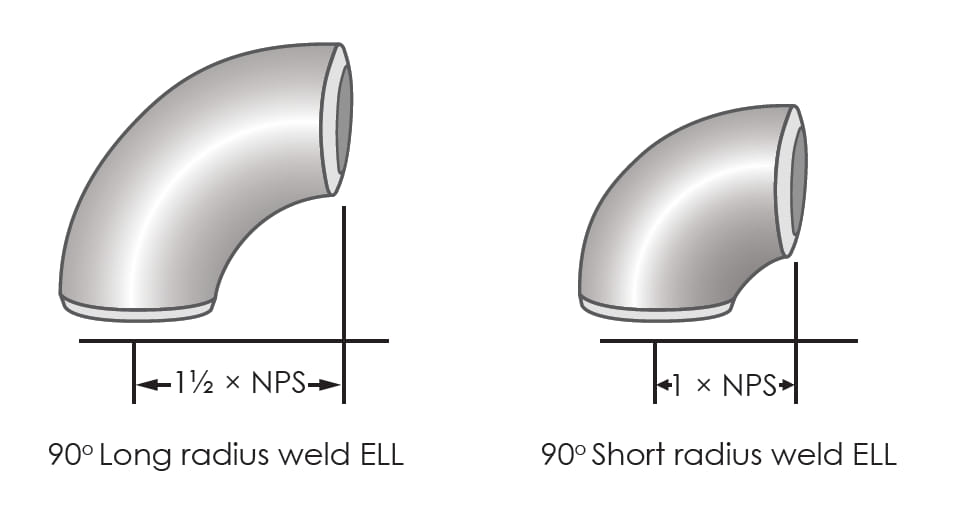
API 5L steel pipe bends are critical pressure-containing directional piping components utilized extensively across international cross-country oil, gas, water, and slurry transportation infrastructure. Unlike standard short-radius (1.0D) or long-radius (1.5D) cold-formed elbows, induction bends are manufactured using continuous medium-frequency induction heating technology. This process allows for large-radius directional shifts (typically 3D, 5D, 6D, 8D, 10D, up to 12D or custom radii) that significantly minimize friction loss, erosion-corrosion, turbulence, and fluid pressure drop inside high-pressure pipeline networks.
The hot induction bending technique involves passing a continuous length of seamless or welded carbon/alloy steel pipe through an electromagnetic induction heating coil. The coil heats a narrow circumferential band (360 degrees around the pipe) to elevated forging temperatures, generally between 850°C and 1050°C (1562°F to 1922°F). As the pipe is pushed forward at a constant controlled velocity by a hydraulic ram, a pivoting mechanical arm clamps the leading edge, applying a bending moment that shapes the pipe around a predetermined center-line radius (CLR). Immediately after leaving the induction coil, the heated zone is quenched using pressurized water spray, forced air, or allowed to cool in still air depending on metallurgical specifications and heat treatment requirements.
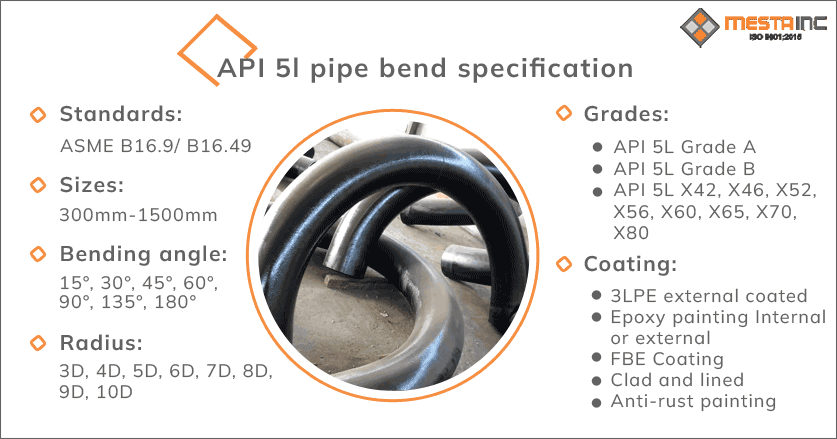
Our facility produces high-grade API 5L X42 through X80 hot induction bends engineered in strict compliance with ANSI/ASME B16.49, ISO 15590-1, and ASME B16.9 standard dimensions. Below is the master specification overview table detailing available sizes, schedules, radii, and value-added processing services.
| Parameter Class | Seamless Pipe Bend Range | Welded (LSAW / HSAW / ERW) Bend Range |
|---|---|---|
| Nominal Diameter (NPS) | 1/2″ to 24″ (DN15 – DN600) | 2″ to 60″ (DN50 – DN1500) |
| Wall Thickness / Schedule | SCH 20, SCH 40, SCH 80, SCH 120, SCH 160, SCH XXS | SCH 10 to SCH 120, WT up to 60 mm (2.36 in) |
| Centerline Bending Radii | 1.5D, 2.5D, 3D, 4D, 5D, 6D, 7D, 8D, 10D, 12D | 3D, 5D, 6D, 7D, 8D, 10D, 12D, Custom CLR up to 15m |
| Bend Angles (θ) | 11.25°, 22.5°, 30°, 45°, 60°, 90°, 180° or Custom | 11.25°, 22.5°, 30°, 45°, 60°, 90°, 180° or Custom |
| Tangent Ends Length (L1, L2) | Standard 100 mm to 500 mm or tailored to site length | Standard 150 mm to 1000 mm or extended tangent options |
| End Preparation | Beveled Ends to ASME B16.25, Plain End Square Cut | Beveled Ends (Compound Bevel / Compound Transition) |
| Surface Protection | Black Vanish, Anti-Rust Oil, FBE, 3LPE, 3LPP, Liquid Epoxy | Blast Cleaning (Sa 2.5), 3LPE Coating, Heavy FBE, Coal Tar |
| Testing Certificates | EN 10204 3.1 / 3.2, 100% UT, RT, MPI, Hydrostatic Test | EN 10204 3.1 / 3.2, 100% Weld Seam RT/UT, Hardness Map |
In high-pressure pipeline design, calculating exact arc length, bend allowance, wall thinning rates, and tangent requirements is vital to prevent material starvation and excessive ovality. The mathematical models governing API 5L hot induction bends are summarized below.
The total arc length required to form a specified bend angle θ with centerline radius R, material thickness t, and neutral axis shift factor K is determined by:
Where: BA = Bend Allowance (mm); θ = Bend Angle (Degrees); R = Centerline Radius (mm); K = K-Factor (neutral axis position ratio, typically 0.33 to 0.50 for hot bending); t = Nominal Wall Thickness (mm).
For standard nominal pipe sizes (NPS or D), the radius designation directly scales with outer diameter:
Calculation Example (6″ 5D Bend): Outer Diameter D = 6″ (152.4 mm). Centerline Radius R = 5 × 6″ = 30″ = 762.0 mm. Total Arc Length for a 90° bend = 90 × (3.14159 / 180) × 762.0 mm = 1196.9 mm (plus tangent lengths).
During the bending process, the outer curve (extrados) experiences tensile strain resulting in wall thinning, while the inner curve (intrados) experiences compressive stress causing wall thickening. To satisfy ASME B31.4 / B31.8 design pressure requirements, the initial pipe wall thickness tnom must be selected so that:
Where tmin is the minimum required pipe wall thickness per line pipe design pressure calculations.
API 5L Grade X60 (equivalent to ISO 3183 L415) PSL1 represents standard quality high-yield seamless and welded line pipe bends designed for non-sour transportation environments. The tables below outline the chemical limit values and minimum required tensile properties.
| Manufacturing Type | Steel Grade | C max | Mn max | P max | S max | V max | Nb max | Ti max | Notes |
|---|---|---|---|---|---|---|---|---|---|
| Seamless Pipe | L415 or X60 | 0.28 | 1.40 | 0.030 | 0.030 | Footnote f | Footnote f | Footnote f | Cu ≤ 0.50%, Ni ≤ 0.50% |
| Welded Pipe | L415 or X60 | 0.26 | 1.40 | 0.030 | 0.030 | Footnote f | Footnote f | Footnote f | Cr ≤ 0.50%, Mo ≤ 0.15% |
Footnotes: (b) For each reduction of 0.01% below carbon max, Mn increase of 0.05% above max is permissible up to 1.75%. (c) Unless agreed, Nb + V ≤ 0.06%. (d) Nb + V + Ti ≤ 0.15%. (f) Unless agreed, Nb + V + Ti ≤ 0.001%. (g) No deliberate addition of Boron (B ≤ 0.001%).
| Steel Grade | Pipe Body (Seamless & Welded) | Weld Seam (EW, SAW, COW) | ||
|---|---|---|---|---|
| Yield Strength Rt0.5 (MPa / psi) min | Tensile Strength Rm (MPa / psi) min | Elongation Af (%) min | Tensile Strength Rm (MPa / psi) min | |
| L415 or X60 | 415 MPa (60,200 psi) | 520 MPa (75,400 psi) | Equation Derived (Af) | 520 MPa (75,400 psi) |
The specified minimum elongation (Af) in percent for API 5L bends is determined using the ISO/API empirical formula based on cross-sectional test piece area:
PSL2 line pipe bends enforce stringent quality criteria, mandatory Carbon Equivalent limits, specified maximum yield strengths, notch toughness Charpy impact testing, and explicit mandatory supply delivery conditions: Normalized (N), Quenched & Tempered (Q), or Thermo-Mechanical Rolled (M).
| Steel Grade | Element Mass Fraction (%) max | Carbon Equivalent max | |||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|
| C | Si | Mn | P | S | V | Nb | Ti | Other | CEIIW | CEPcm | |
| L415N or X60N (SMLS) | 0.24 | 0.45 | 1.40 | 0.025 | 0.015 | 0.10 | 0.05 | 0.04 | g, h, l | As Agreed | As Agreed |
| L415Q or X60Q (SMLS) | 0.18 | 0.45 | 1.70 | 0.025 | 0.015 | g | g | g | h, l | 0.43 | 0.25 |
| L415M or X60M (Welded) | 0.12 | 0.45 | 1.60 | 0.025 | 0.015 | g | g | g | h, l | 0.43 | 0.25 |
CE Formulas: CEIIW = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15 | CEPcm = C + Si/30 + (Mn+Cu+Cr)/20 + Ni/60 + Mo/15 + V/10 + 5B.
| Steel Grade | Pipe Body Requirements | Weld Seam | |||
|---|---|---|---|---|---|
| Yield Strength Rt0.5 (MPa) min / max | Tensile Strength Rm (MPa) min / max | Ratio Rt0.5 / Rm max | Elongation Af (%) min | Tensile Strength Rm (MPa) min | |
| L415N / X60N | 415 MPa (60,200 psi) min 565 MPa (81,900 psi) max |
520 MPa (75,400 psi) min 760 MPa (110,200 psi) max |
0.93 | Formula Derived | 520 MPa (75,400 psi) |
| L415Q / X60Q | |||||
| L415M / X60M | |||||
Pipeline networks conveying wet hydrogen sulfide (H2S) gas or crude oil demand specialized sour service resistant pipe bends. Sour service bends are strictly controlled to prevent Hydrogen-Induced Cracking (HIC), Sulfide Stress Cracking (SSC), and Stepwise Cracking (SWC) under NACE MR0175 / ISO 15156 compliance.
| Steel Grade | C max | Si max | Mn max | P max | S max | V max | Nb max | Ti max | CEIIW max | CEPcm max |
|---|---|---|---|---|---|---|---|---|---|---|
| L415QS / X60QS (SMLS) | 0.16 | 0.45 | 1.65 | 0.020 | 0.003 | 0.08 | 0.05 | 0.04 | 0.41 | 0.22 |
| L415MS / X60MS (Welded) | 0.10 | 0.45 | 1.45 | 0.020 | 0.002 | 0.08 | 0.08 | 0.06 | — | 0.21 |
Critical Sour Controls: Ultra-low Sulfur (S ≤ 0.002% for welded, 0.003% for seamless). Calcium treatment for inclusion shape control (Ca/S ≥ 1.5). Hardness limit: Maximum 22 HRC (238 HBW) across base metal, heat-affected zone (HAZ), and weld seam.
| Steel Grade | Yield Strength Rt0.5 (MPa) min / max | Tensile Strength Rm (MPa) min / max | Yield-to-Tensile Ratio max | Hardness Cap (HRC) | HIC / SSC Testing |
|---|---|---|---|---|---|
| L415QS / X60QS | 415 MPa (60,200 psi) min 565 MPa (81,900 psi) max |
520 MPa (75,400 psi) min 760 MPa (110,200 psi) max |
0.93 | 22 HRC (238 HBW) |
NACE TM0284 (HIC) NACE TM0177 (SSC) |
| L415MS / X60MS |
ASME B16.49 is the definitive standard governing the design, material qualification, manufacturing processes, testing, marking, and inspection requirements for factory-made pipeline bends made from carbon and low-alloy steel materials with controlled chemistry and mechanical properties. It specifically covers induction bends for pipeline transportation and distribution piping systems compliant with ASME B31.4 (Liquid Hydrocarbons) and ASME B31.8 (Gas Transmission).
| Element | Carbon [C] | Manganese [Mn] | Phosphorus [P] | Sulfur [S] | Silicon [Si] | Chromium [Cr] | Molybdenum [Mo] |
|---|---|---|---|---|---|---|---|
| Max Content (%) | 0.30 | 1.60 | 0.025 | 0.015 | 0.50 | 0.30 | 0.25 |
| Element | Vanadium [V] | Copper [Cu] | Nickel [Ni] | Niobium [Nb] | Carbon Equivalent Formula (C.E.) | ||
| Max Content (%) | 0.10 | 0.50 | 1.00 | 0.10 | C.E. = C + Mn/6 + (Cr+Mo+V)/5 + (Cu+Ni)/15 ≤ 0.45% | ||
Under ASME B16.49, induction bends are designated by standard grade symbols matching their minimum yield strength in megapascals (MPa). The table below lists the mechanical baseline properties, hardness thresholds, and Charpy V-Notch (CVN) impact toughness values required post-bending.
| Grade Symbol | Equivalent API 5L Grade | Yield Strength min | Tensile Strength min | Elongation min | Max Hardness | Impact Test (Cv) | |||
|---|---|---|---|---|---|---|---|---|---|
| ksi | MPa | ksi | MPa | % | HBW | HRC | Joules (min avg) | ||
| P241 (X241) | Grade B / L245 | 35 | 241 | 60 | 414 | 20 | 238 | 22 | 27 J @ -20°C |
| P290 (X290) | X42 / L290 | 42 | 290 | 60 | 414 | 20 | 238 | 22 | 27 J @ -20°C |
| P317 (X317) | X46 / L320 | 46 | 317 | 63 | 434 | 20 | 238 | 22 | 27 J @ -20°C |
| P359 (X359) | X52 / L360 | 52 | 359 | 66 | 455 | 20 | 238 | 22 | 27 J @ -20°C |
| P386 (X386) | X56 / L390 | 56 | 386 | 71 | 490 | 20 | 238 | 22 | 27 J @ -20°C |
| P414 (X414) | X60 / L415 | 60 | 414 | 75 | 517 | 20 | 238 | 22 | 54 J @ -20°C |
| P448 (X448) | X65 / L450 | 65 | 448 | 77 | 531 | 18 | 238 | 22 | 54 J @ -20°C |
| P483 (X483) | X70 / L485 | 70 | 483 | 82 | 565 | 16 | 247 | 24 | 54 J @ -20°C |
| P552 (X552) | X80 / L555 | 80 | 552 | 90 | 621 | 16 | 247 | 24 | 54 J @ -20°C |
Because hot induction bending subjects the steel pipe to rapid localized thermal cycles, full post-bending heat treatment (PBHT) is mandatory to restore fine-grained microstructure, relieve residual bending stresses, and guarantee notch toughness across base metal, bend zone, and weld seams.
Uniformly heat the bend between 480°C (900°F) and 675°C (1250°F). Hold at temperature for at least 30 minutes per 25 mm (1 in.) of wall thickness, but no less than 30 minutes total. Air cool in still air.
Heat uniformly above the upper transformation temperature (Ac3, typically 880°C–930°C). Hold for a minimum of 20 minutes per 25 mm (1 in.) of thickness, then cool freely in still air to achieve uniform ferrite-pearlite structure.
Heat above transformation temperature, hold for 20 min/25 mm, then rapidly quench in water, oil, or polymer quenchant. Reheat for high-temperature tempering (550°C–650°C) to attain optimal yield strength and impact toughness.
The table below provides center-to-end (A, B) and back-to-face (O, K) dimensions for standard 3D and Long Radius (LR) pipe bends across nominal pipe sizes DN15 (1/2″) to DN400 (16″) in accordance with ASME B16.49 and ASME B16.9.
| DN | NPS | Outside Dia (OD) | Center to End (90° Bend) A | Center to End (45° Bend) B | Back to Face (180° Return) O | Center to Center (180° Return) K | ||||
|---|---|---|---|---|---|---|---|---|---|---|
| 3D Bend | LR Bend | 3D Bend | LR Bend | 3D Bend | LR Bend | 3D Bend | LR Bend | |||
| 15 | 1/2″ | 21.3 | 76 | 38 | 48 | 22 | 203 | 102 | 76 | 38 |
| 20 | 3/4″ | 26.7 | 76 | 38 | 57 | 25 | 247 | 127 | 76 | 38 |
| 25 | 1″ | 33.4 | 76 | 38 | 63 | 29 | 176 | 102 | 76 | 51 |
| 32 | 1 1/4″ | 42.2 | 95 | 48 | 39 | 24 | 95 | 102 | 64 | 64 |
| 40 | 1 1/2″ | 48.3 | 114 | 57 | 47 | 29 | 114 | 127 | 76 | 76 |
| 50 | 2″ | 60.3 | 152 | 76 | 63 | 35 | 152 | 152 | 102 | 102 |
| 65 | 2 1/2″ | 73.0 | 190 | 95 | 79 | 44 | 190 | 190 | 127 | 127 |
| 80 | 3″ | 88.9 | 229 | 114 | 95 | 51 | 229 | 229 | 152 | 152 |
| 90 | 3 1/2″ | 101.6 | 267 | 133 | 111 | 57 | 267 | 267 | 178 | 178 |
| 100 | 4″ | 114.3 | 305 | 152 | 127 | 64 | 305 | 305 | 203 | 203 |
| 125 | 5″ | 141.3 | 381 | 190 | 157 | 79 | 381 | 381 | 254 | 254 |
| 150 | 6″ | 168.3 | 457 | 229 | 189 | 95 | 457 | 457 | 305 | 305 |
| 200 | 8″ | 219.1 | 610 | 305 | 252 | 127 | 610 | 610 | 406 | 406 |
| 250 | 10″ | 273.0 | 762 | 381 | 316 | 159 | 762 | 762 | 508 | 508 |
| 300 | 12″ | 323.8 | 914 | 457 | 378 | 191 | 914 | 914 | 609 | 609 |
| 350 | 14″ | 355.6 | 1067 | 533 | 441 | 222 | 1067 | 1067 | 711 | 711 |
| 400 | 16″ | 406.4 | 1219 | 610 | 505 | 254 | 1219 | 1219 | 813 | 813 |
Selecting the proper steel grade for cross-country pipeline bends requires balancing operational pressure requirements, field weldability, fracture toughness, and cost effectiveness. The comparison tables below evaluate chemical limits and mechanical thresholds across the high-yield API 5L spectrum.
| Grade | Carbon [C] | Silicon [Si] | Manganese [Mn] | Phosphorus [P] | Sulfur [S] | Vanadium [V] | Niobium [Nb] | Titanium [Ti] |
|---|---|---|---|---|---|---|---|---|
| API 5L X52 | 0.16 | 0.45 | 1.65 | 0.020 | 0.010 | 0.07 | 0.05 | 0.04 |
| API 5L X56 | 0.16 | 0.45 | 1.65 | 0.020 | 0.010 | 0.07 | 0.05 | 0.04 |
| API 5L X60 | 0.16 | 0.45 | 1.65 | 0.020 | 0.010 | 0.08 | 0.05 | 0.04 |
| API 5L X65 | 0.16 | 0.45 | 1.65 | 0.020 | 0.010 | 0.09 | 0.05 | 0.06 |
| API 5L X70 | 0.17 | 0.45 | 1.75 | 0.020 | 0.010 | 0.10 | 0.05 | 0.06 |
| Grade | Yield Strength min (KSI / MPa) | Tensile Strength min (KSI / MPa) | Yield-to-Tensile Ratio max | Elongation min (%) |
|---|---|---|---|---|
| API 5L X52 | 52 KSI / 359 MPa | 66 KSI / 455 MPa | 0.93 | 21 % |
| API 5L X56 | 56 KSI / 386 MPa | 71 KSI / 490 MPa | 0.93 | 19 % |
| API 5L X60 | 60 KSI / 414 MPa | 75 KSI / 517 MPa | 0.93 | 19 % |
| API 5L X65 | 65 KSI / 448 MPa | 77 KSI / 531 MPa | 0.93 | 18 % |
| API 5L X70 | 70 KSI / 483 MPa | 82 KSI / 565 MPa | 0.93 | 17 % |
To ensure structural integrity under severe cyclic pressure and environmental loads, 100% of manufactured hot induction bends undergo exhaustive non-destructive examination (NDE) and destructive metallurgical testing in full accordance with ASME B16.49 Clause 10 and ISO 15590-1.
| Testing Method | Standard / Specification | Acceptance Criteria & Inspection Scope |
|---|---|---|
| Ultrasonic Testing (UT) | ASTM A388 / ASME Sec V Art 4 | 100% full body wall thickness measurement post-bending; 100% shear wave UT of bend intrados/extrados and weld seam. |
| Radiographic Testing (RT) | ASME Sec V Art 2 / API 1104 | 100% X-ray examination of circumferential and longitudinal weld seams on welded pipe bends post-forming. |
| Magnetic Particle Inspection (MPI) | ASTM E709 / ASME Sec V Art 7 | 100% wet magnetic particle inspection of bevel ends, intrados, extrados, and body to detect surface/sub-surface cracks. |
| Hardness Testing & Mapping | ASTM E10 (Brinell) / ASTM E18 (Rockwell) | Grid mapping across outer radius, inner radius, neutral axis, and weld/HAZ zones. Max 238 HBW (22 HRC for sour service). |
| Charpy V-Notch (CVN) Impact | ASTM A370 / ISO 148-1 | Impact testing at -20°C (-4°F) or -46°C (-51°F). Minimum individual energy per ASME B16.49 baseline table. |
| Hydrostatic Testing | API 5L Clause 10.2 / ASME B31.8 | Test pressure maintained for minimum 10 seconds without body or seam leakage at calculated hoop stress (90% SMYS). |
Hot induction bends placed in underground, subsea, or above-ground pipeline environments require specialized anti-corrosion coating systems capable of conforming to curved bend geometries without disbondment.
Tight geometric tolerances are crucial for maintaining line pipe fit-up, minimizing offset during field automatic girth welding, and avoiding stress concentration points.
| Dimensional Feature | Nominal Diameter Range | Permissible Tolerance Limit |
|---|---|---|
| Bend Angle (θ) Tolerance | All Sizes (1/2″ to 60″) | ±0.5° of specified bend angle |
| Centerline Radius (CLR) Tolerance | All Sizes | ±1.0% of specified centerline radius R |
| Outside Diameter (OD) at Ends | NPS ≤ 4″ NPS 5″ to 12″ NPS ≥ 14″ |
+1.6 mm / -0.8 mm ±1.6 mm +2.4 mm / -1.6 mm |
| Ovality (Out-of-Roundness) in Bend | All Sizes | Max 3.0% [(ODmax – ODmin) / ODnom × 100] |
| End Squareness / Bevel Angle | All Sizes | Bevel angle 37.5° ± 2.5°; Root face 1.6 mm ± 0.8 mm; Off-square ≤ 1.6 mm |
| Tangent Length (L1, L2) Tolerance | All Sizes | ±5.0 mm or as agreed upon between purchaser and manufacturer |
To expedite quotation and ensure flawless engineering compliance, engineering procurement contracts (EPC) should incorporate the full technical profile when requesting quotations for hot induction bends.
Long Weld Neck Flanges (LWN)
WP304 pipe Accessories Stocks
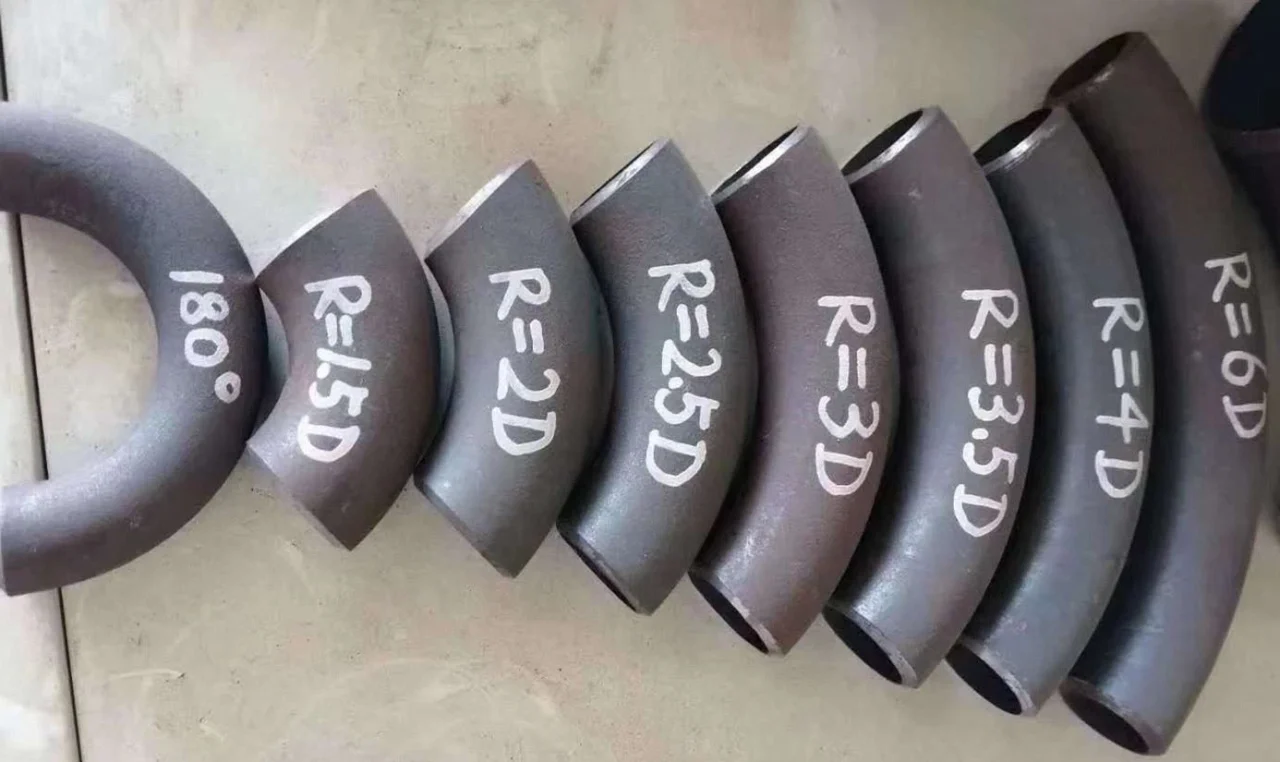
As a dedicated manufacturer of pipe fittings, we pride ourselves on delivering ASME/ANSI B16.9 Long Radius Elbows that meet the strictest international standards. The dimensions and weights provided in this guide are a testament to our commitment to precision and quality. Whether your project requires a small NPS 1/2 fitting for a pharmaceutical plant or a massive NPS 48 elbow for an offshore platform, our products are engineered for a perfect fit and long-lasting service. For further technical assistance, custom inquiries, or to request a formal quotation, please contact our engineering sales team.
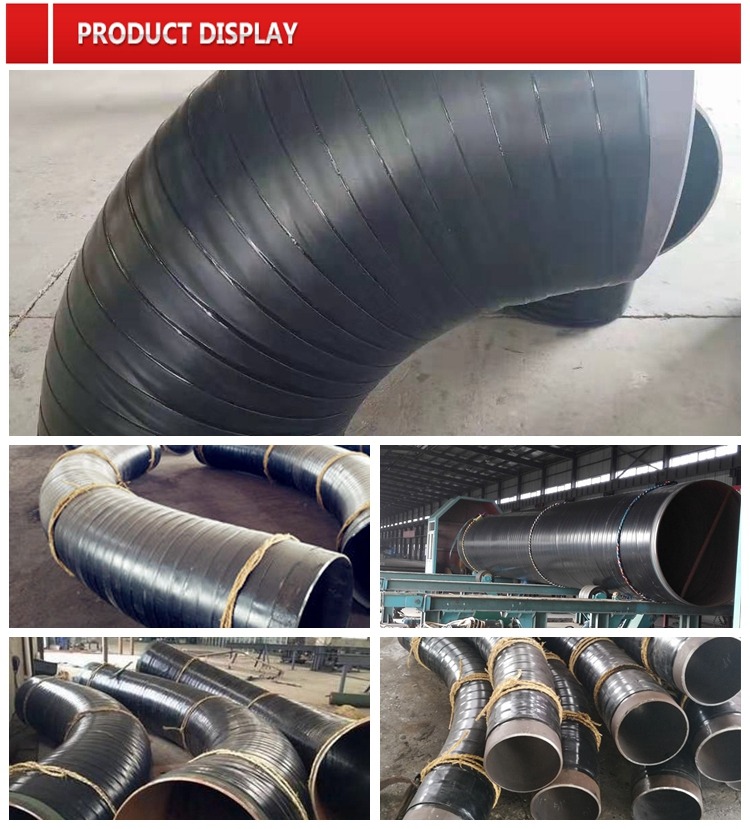
Our product, the API 5L X52 and X60 Hot Induction Steel Pipe Bend, available in crucial 5D,8D, and 10D radii, is the embodiment of advanced thermal-mechanical processing applied to high-strength metallurgy. I
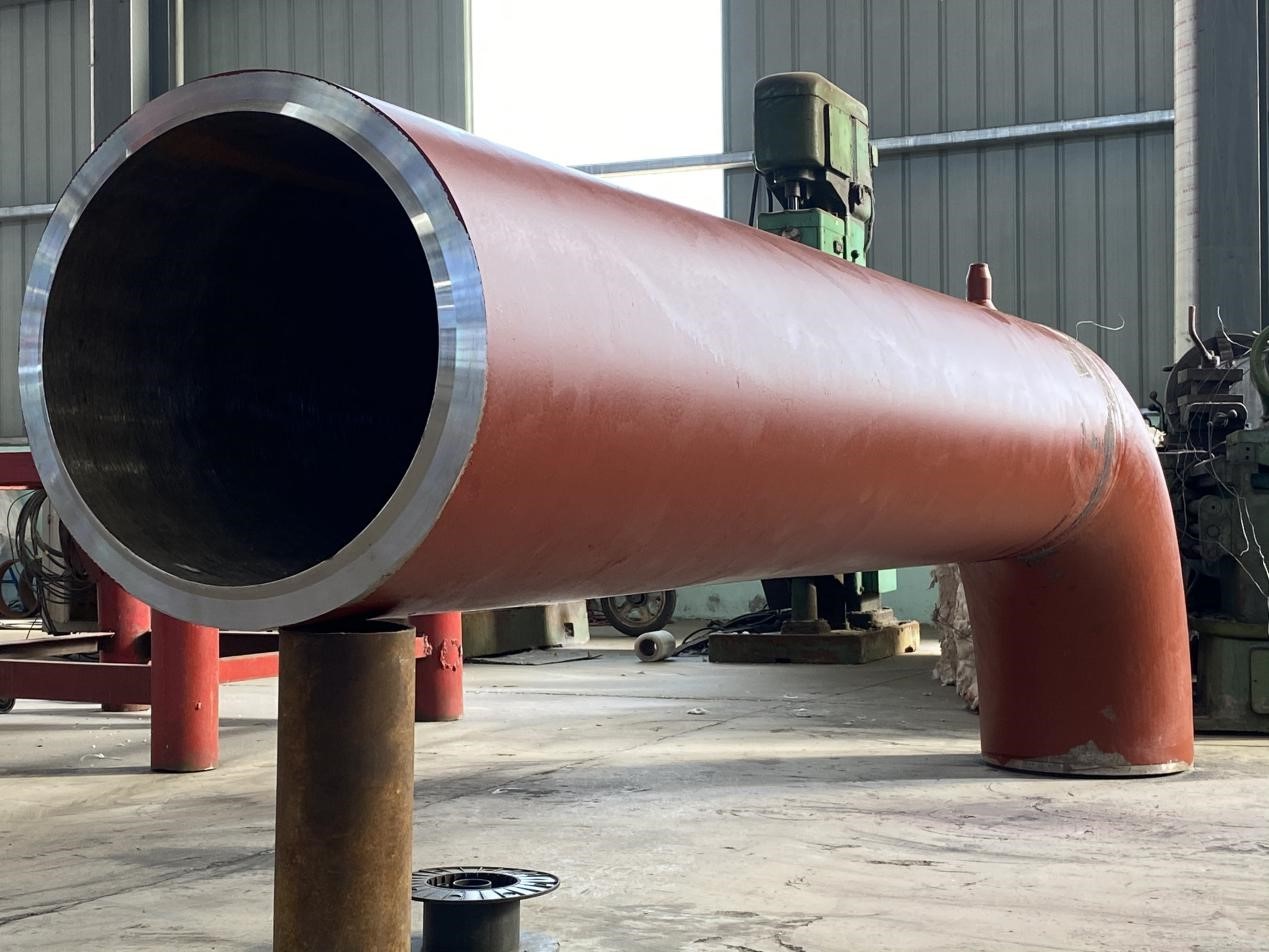
Piping spool fabrication is a sophisticated process that combines engineering precision, materials science, and advanced manufacturing techniques to deliver high-quality, modular piping systems. By controlling key parameters like pipe diameter, material selection, and weld quality, fabricators ensure spools meet stringent industry standards like ASME B31.3 and API 1104. Advances in automation, digital tools, and sustainable practices are transforming the industry, enabling faster, greener, and more cost-effective production.
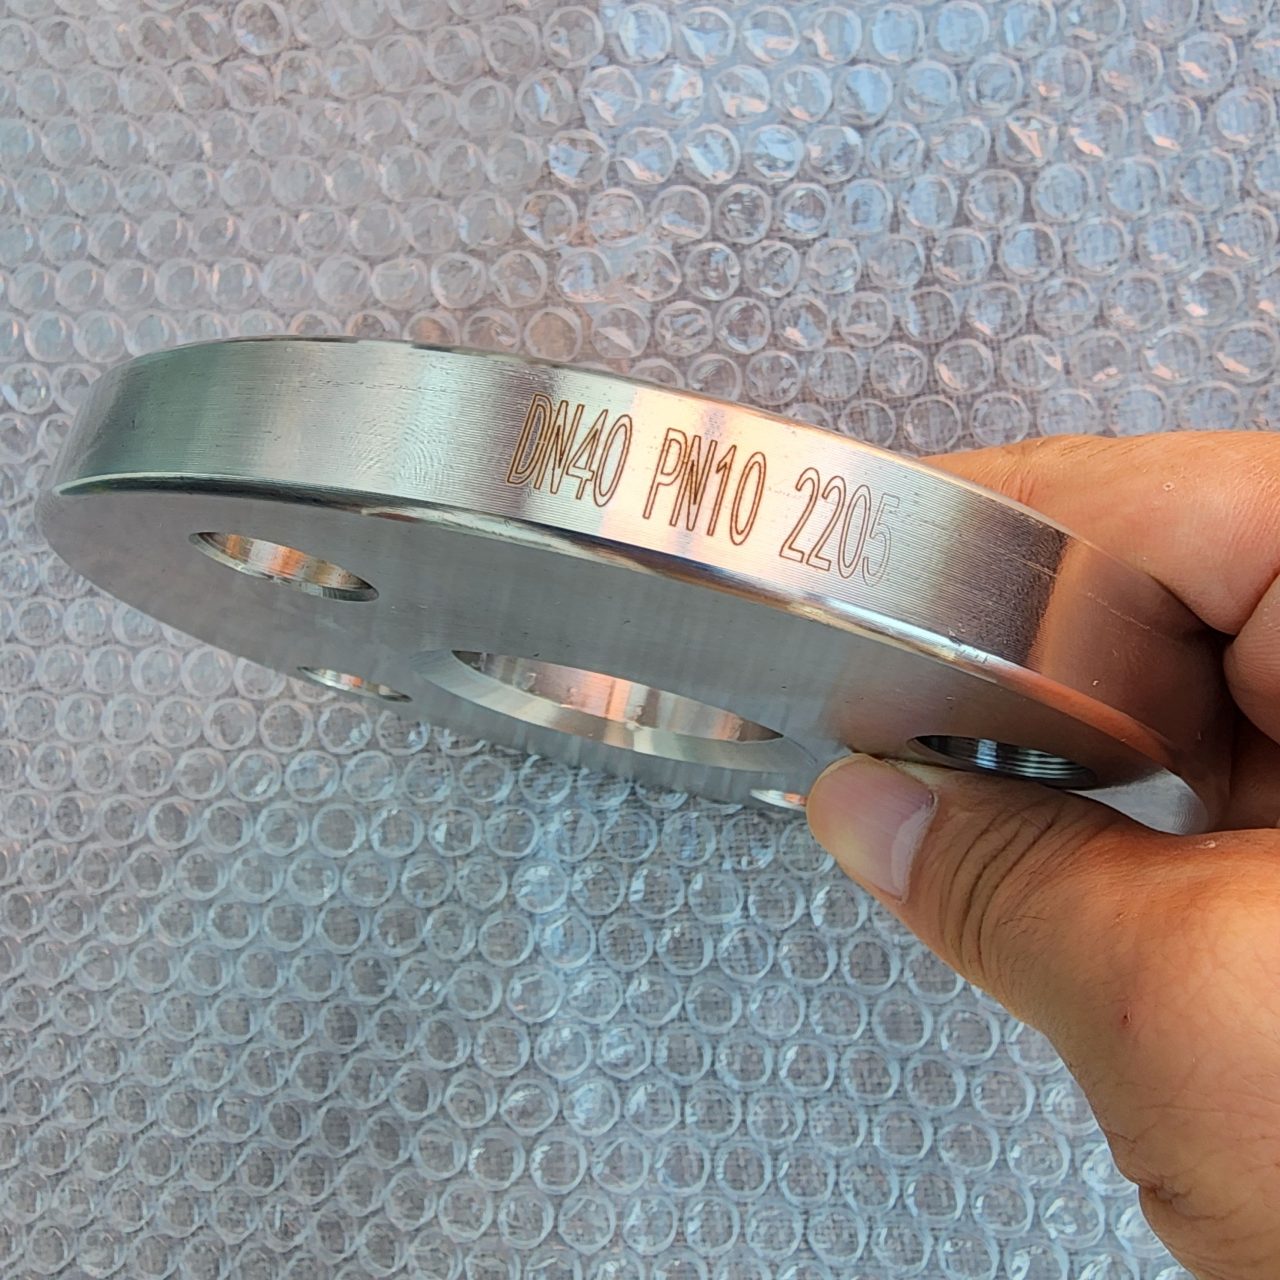
2205 duplex steel plate flat welding flange (HG/T 20592 DN40 PN10 PLRF) combines the corrosion resistance of the material with the lightweight advantages of the structure, and is suitable for medium and low pressure corrosive environments such as chemical industry and marine engineering. Its design must strictly follow the size and pressure specifications of HG/T 20592, and pay attention to the welding process and maintenance requirements during processing and use to ensure long-term reliability.
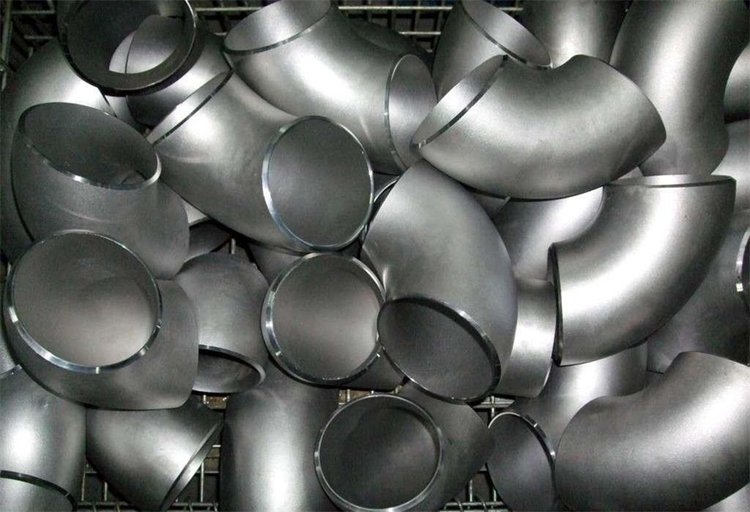
Monel K-500 is a high-performance nickel-copper-based alloy with excellent corrosion resistance and mechanical properties, suitable for a variety of industrial applications. Its good welding properties and processability make it have high flexibility in the manufacturing process. Through appropriate heat treatment processes, its performance can be further improved and the needs of different working conditions can be met.
Abter Company use Steel grade :GB 18248 37Mn, 34Mn2V, 30CrMo, 35CrMo, 34CrMo4, 30CrMnSiA / JIS G3429STH11, STH12, STH21, STH22, STH31 of steel to produce gas cylinder steel tubes
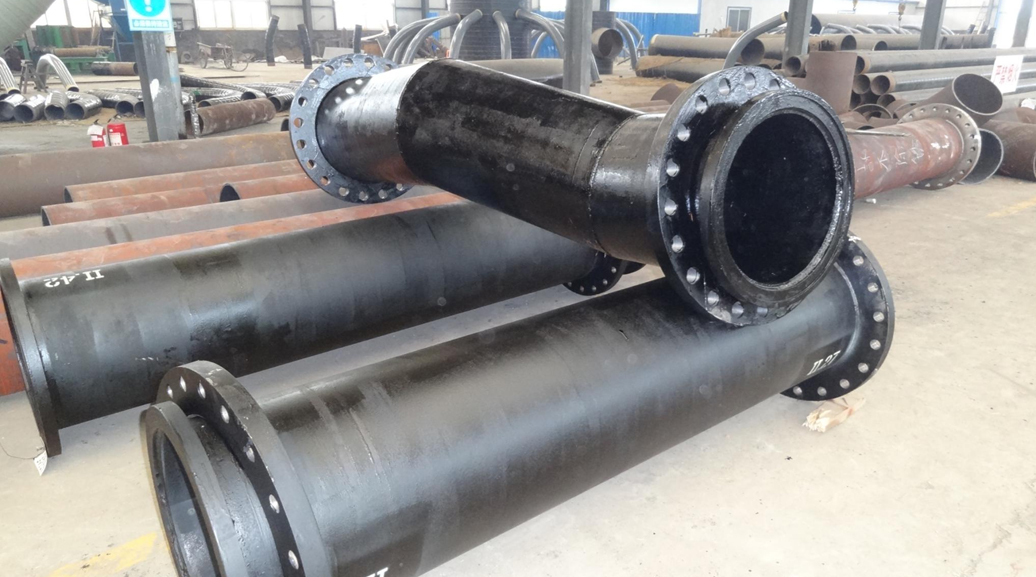
WHAT IS PIPE PREFABRICATION? Pipe prefabrication is manufacturing pieces of pipelines in a factory instead at the construction site. This enables utilization of better tools and working conditions. This results in higher productivity and better quality. It also reduces the lead time at the construction site.
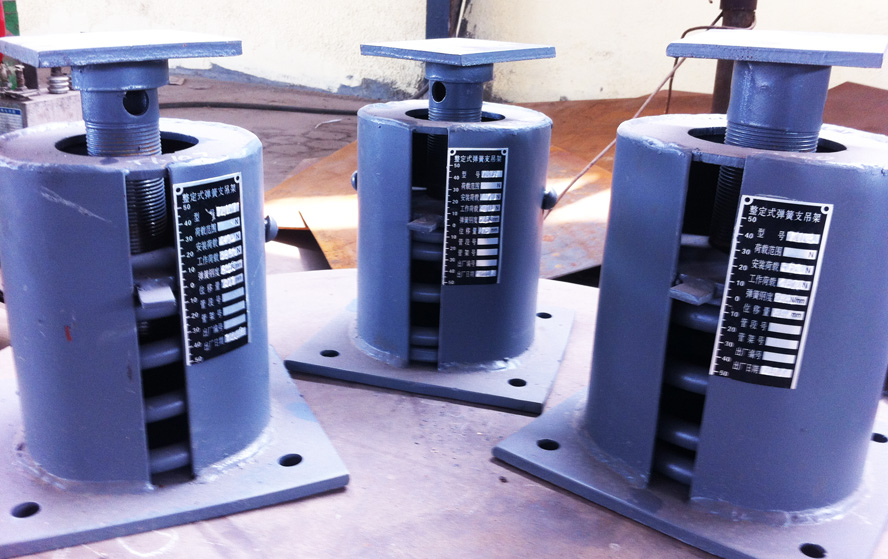
Type A- Used where ample head room is available. Specific elevation is desirable. Type B- Used where headroom is limited. Head attachment is a single lug. Type C- Used where headroom is limited. Head attachment is side by side lugs
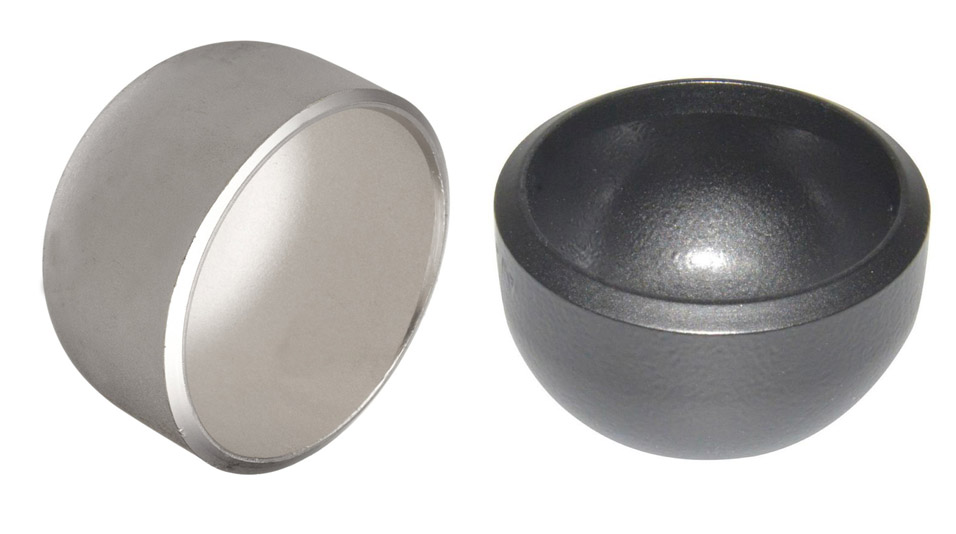
Butt Weld Cap We are manufacturer of butt weld cap and supplies all schedules in kinds of materials such as carbon steel, stainless steel, alloy steel. Zizi produces pipe caps in ASME, DIN, JIS and other required standards. Pipe cap is one of the common used pipe fittings for stoping fluid by covering at the pipe end. It is available in butt weld type, socket weld type and threaded type, and buttweld cap is more popular in view of the good performance, stable connection and large dimension selection range.
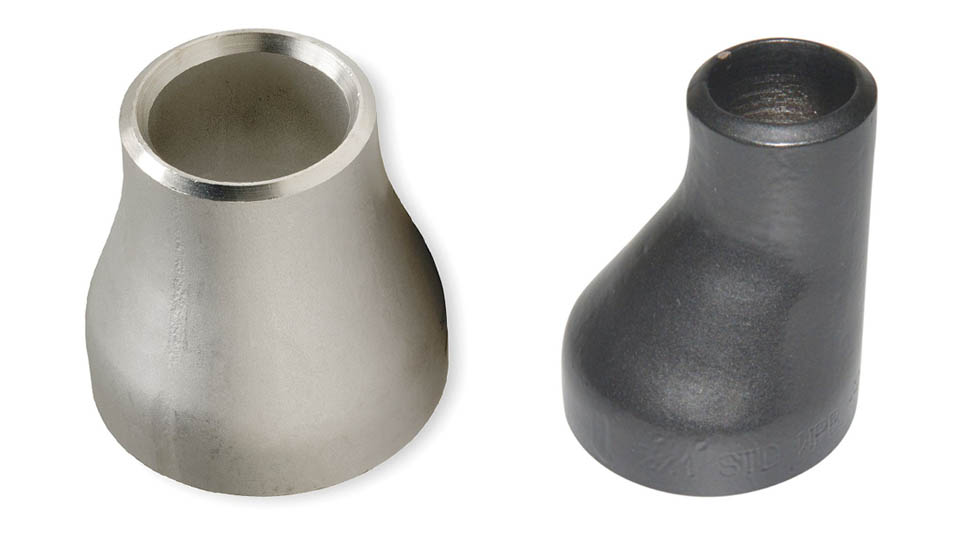
Concentric reducers are used where the pipework is vertically installed and at the discharge side of pumps. Eccentric reducers are more often used when the pipework lays on a pipe rack. Because of the flat side, aligning and securely mounting the pipes to the rack is easier.
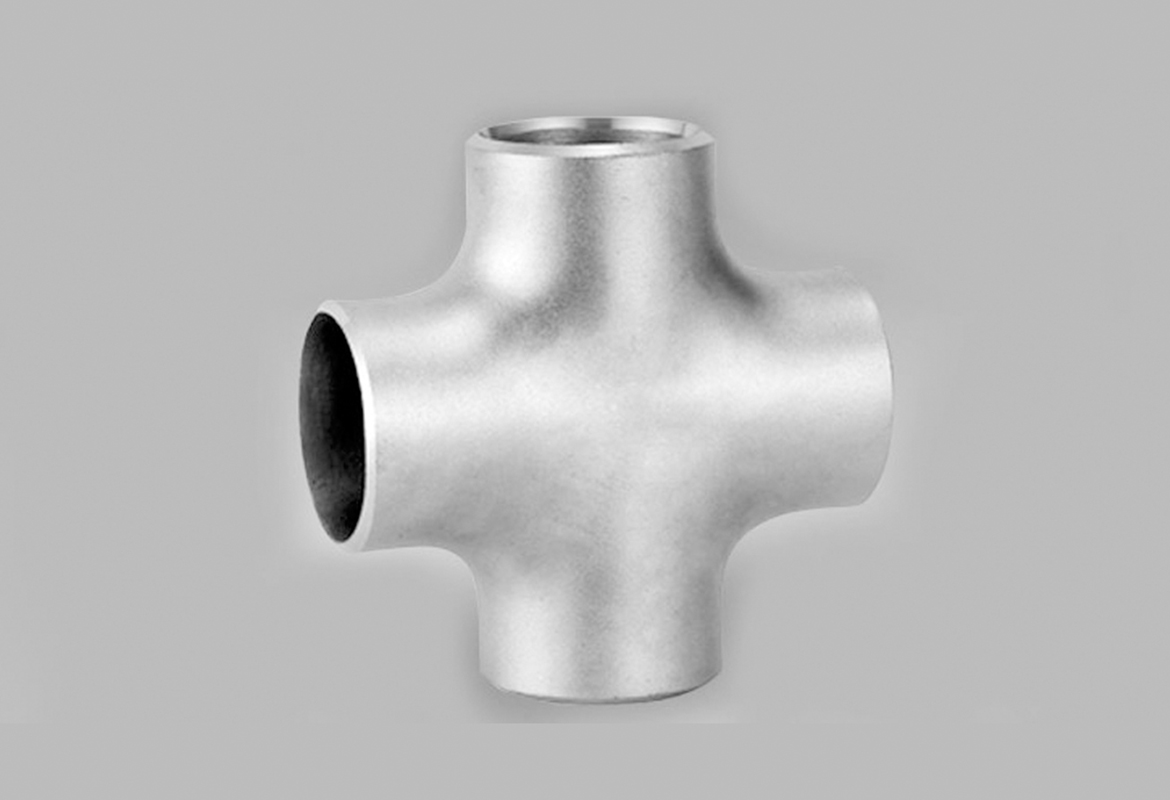
Cross fittings allow for the branching of pipes, enabling the distribution of water or other fluids to various fixtures or areas. They are commonly used in water supply systems, irrigation systems, and heating systems.
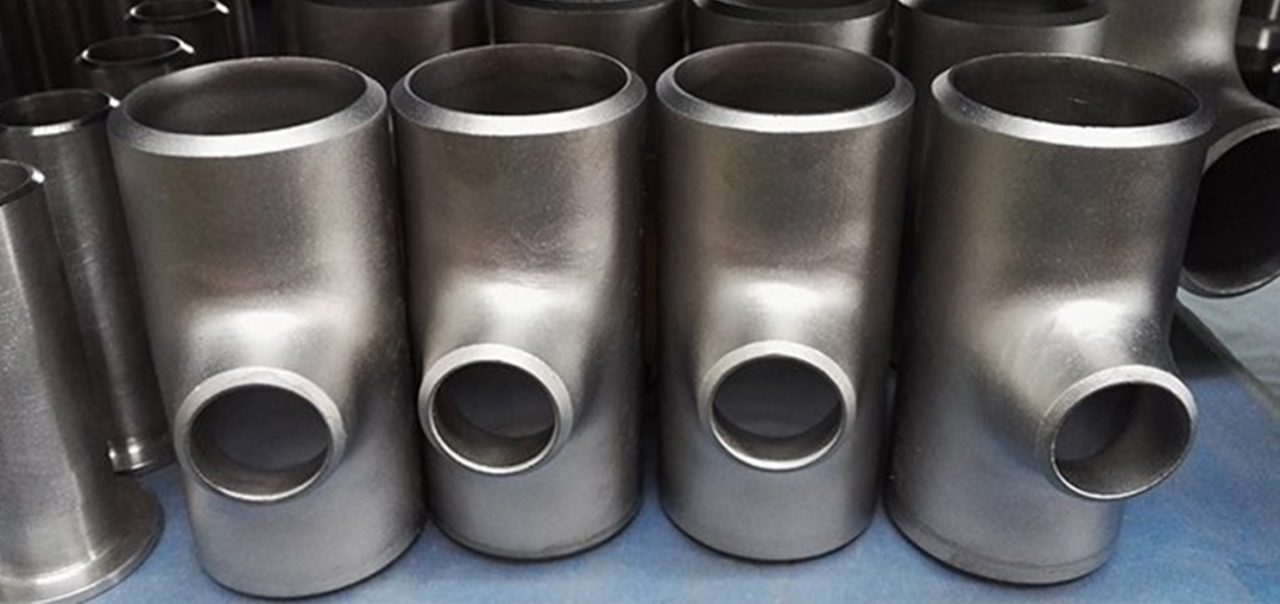
Material Stainless Steel ASME / ASTM SA / A403 SA / A 774 WP-S, WP-W, WP-WX, 304, 304L, 316, 316L, 304/304L, 316/316L, DIN 1.4301, DIN1.4306, DIN 1.4401, DIN 1.4404 Dimension ANSI B16.9, ANSI B16.28, MSS-SP-43 Type A, MSS-SP-43 Type B, JIS B2312, JIS B2313 Thickness Schedule 5S, 10S, 20S, S10, S20, S30, STD, 40S, S40, S60, XS, 80S, S80, S100, S120, S140, S160, XXS and etc.
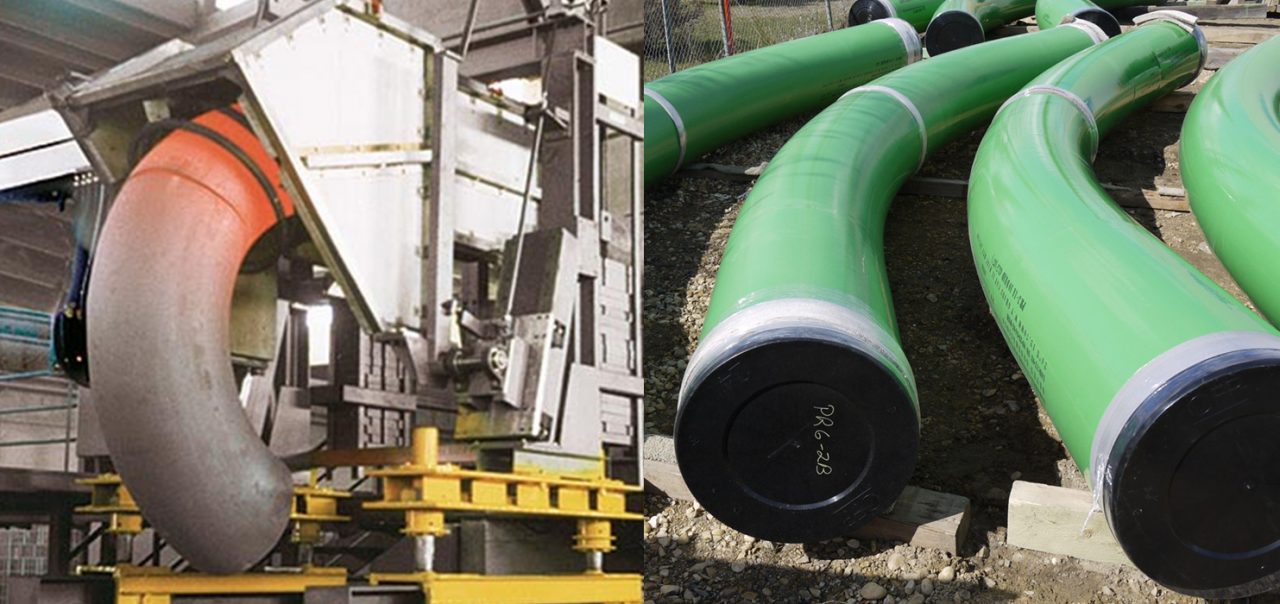
Pipe fitting bodies are usually made of the same base material as the pipe or tubing they are connected to: copper, steel, PVC, CPVC or ABS. Any material permitted by plumbing, health or building codes (as applicable) may be used, but it must be compatible with the other materials in the system, the fluid being conveyed, and the temperature and pressure inside (and outside) the system. Brass or bronze fittings over copper Common in plumbing and plumbing systems. Fire resistance, shock resistance, mechanical strength, anti-theft and other factors also affect the choice of material for pipe fittings.
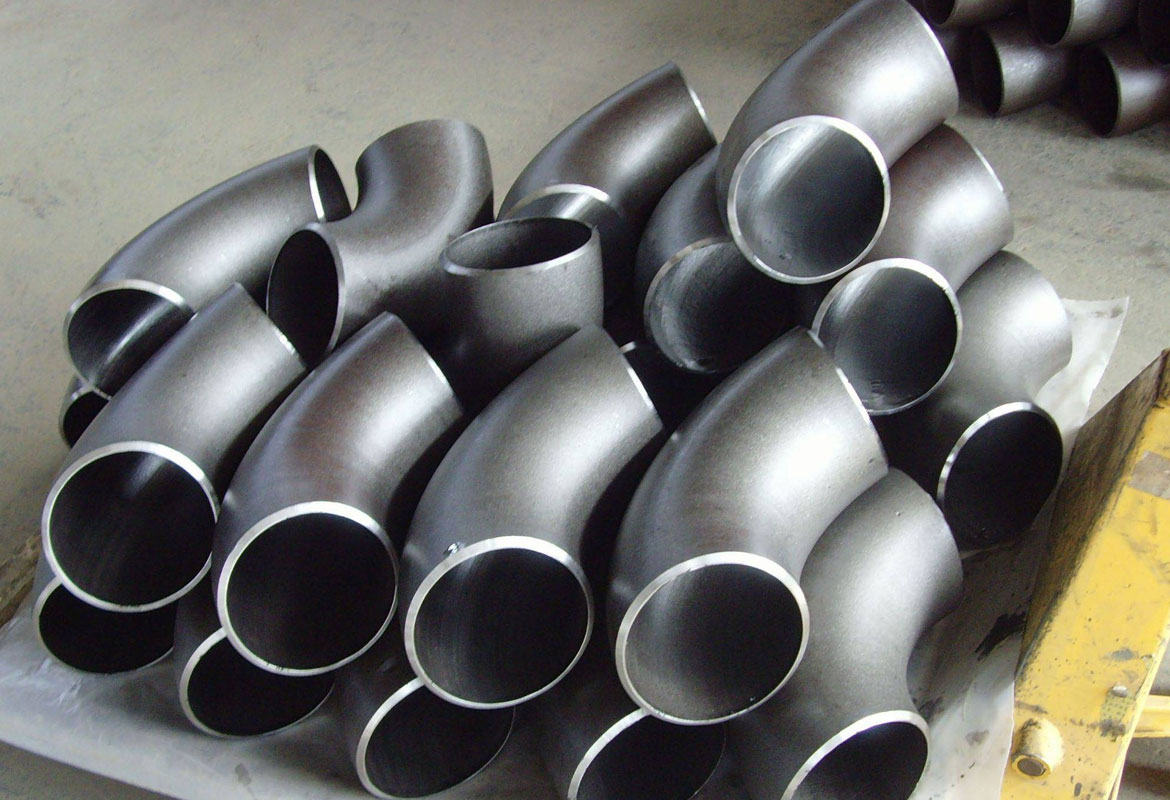
Pipe fittings are used in plumbing systems to connect straight sections of pipe or tubes, to accommodate different sizes or shapes, and for other purposes such as regulating (or measuring) fluid flow. These fittings are used in plumbing systems to control the transfer of water, gas or liquid waste within pipes or plumbing systems in domestic or commercial environments. Fittings (especially uncommon types) require money, time, materials and tools to install and are an important part of plumbing and plumbing systems. Common pipe fittings mainly include: flange, elbows, couplings, unions, spools, reducers, bushings, tees, diverter tees, crosses, caps, plugs, barbs and valves. Although valves are technically fittings, they are usually discussed separately.